1. Bench pickup check
Start with representative parts, including the worst expected surface condition. Check pickup contact, peel risk, air gap, and any stacked-part behavior before approving the gripper concept.
Prototype review, inspection planning, and production-control discussion for repeat magnetic gripper orders.
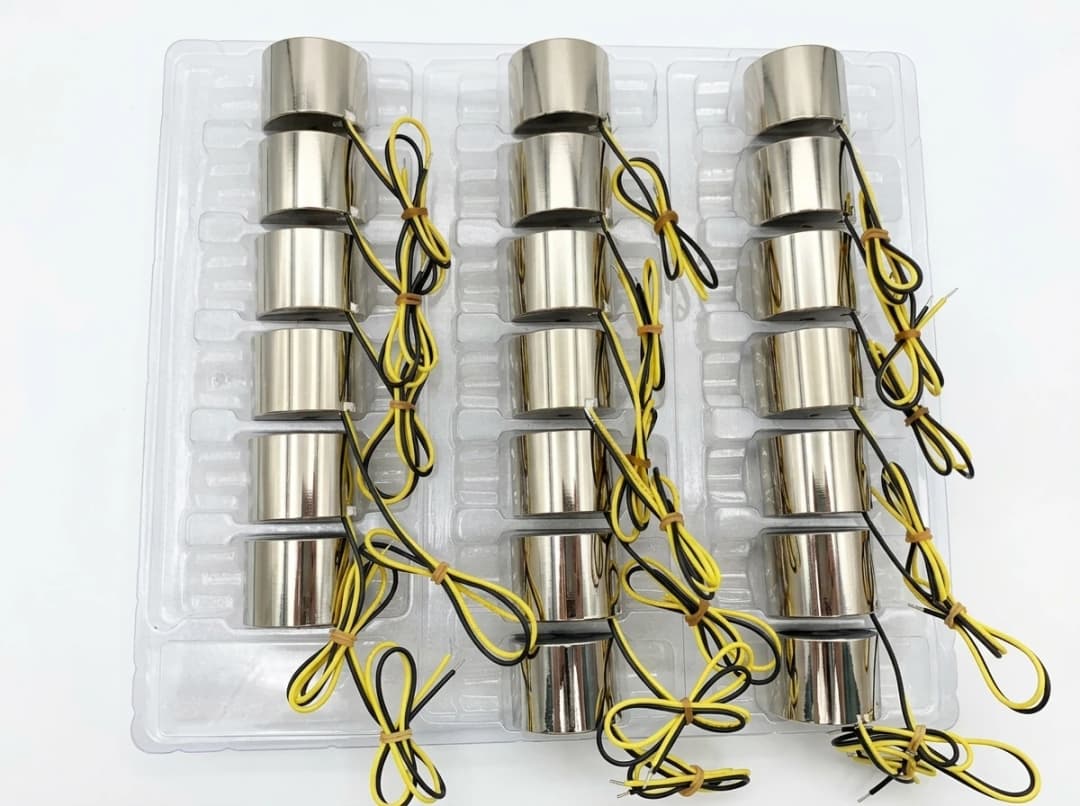
Treat sample validation and quality control as a complete handling decision, not a stand-alone magnet purchase. The right choice depends on whether the workpiece can be held magnetically, whether the robot motion keeps enough margin, whether the part releases cleanly, and whether the installation scope is clear enough for quotation.
Buyer fit: For buyers who need a practical path from concept review to repeatable factory supply. Before comparing price, align the practical constraints below so the quote reflects the real automation cell instead of a generic catalog condition.
| Decision Area | Buyer Question | Practical Evidence |
|---|---|---|
| Workpiece fit | Can the magnetic poles contact enough real surface area under production conditions? | Send prototype quantity, acceptance criteria, and deadline for sample review plus photos or drawings of the pickup face. |
| Motion margin | Will the gripper hold through acceleration, rotation, off center pickup, and stop conditions? | Review validation evidence because sample validation reduces the risk of releasing an unsuitable gripper into production. |
| Release behavior | Can the part release within the placement tolerance without residual magnetism, double pickup, or stack disturbance? | Define sample acceptance criteria around validation evidence and record the release test result before batch release. |
| Interface scope | Are the flange, adapter, cable, connector, controller, and documentation assumptions included in the same RFQ? | Confirm sample acceptance criteria and list any custom mounting or control requirements before PO release. |
Start with representative parts, including the worst expected surface condition. Check pickup contact, peel risk, air gap, and any stacked-part behavior before approving the gripper concept.
Test the planned orientation, acceleration, tool center, cable route, and stop assumptions. A static lift is not enough when the cell includes fast motion or rotated handling.
Measure release timing, residual magnetism, placement tolerance, and repeatability across a small run. Use the result to freeze pole layout, interface, and quality-control notes.
The most common sourcing mistake is treating holding force as a fixed catalog value. In practice, sample is approved under time pressure without testing on worst-case production parts. Include the most challenging workpiece variants (thinnest, oiliest, most burred) in the sample validation set. Another common issue is that batch production drifts from the validated sample because inspection criteria were not documented. Create a formal inspection plan with specific dimensions, tolerances, test methods, and sampling frequency before the first batch.
For a quote that can move from engineering review to procurement, include the workpiece file set, automation interface, cycle target, release requirement, quantity, destination, and any custom packaging or documentation needs. If those values are not final, mark them as assumptions so the quotation can separate confirmed scope from validation-dependent scope.
| Program Metric | Typical Range | Procurement Value |
|---|---|---|
| Validation evidence | Defined by buyer acceptance criteria and sample review | Sample validation reduces the risk of releasing an unsuitable gripper into production. |
Typically 2-5 samples cover initial fit, function, and destructive testing. For statistical validation (Cpk), a larger sample of 30+ may be needed. Define the validation scope before ordering.
We provide inspection reports covering the agreed critical dimensions, plus material certificates and holding force test data. Additional documentation (photos, traceability labels) can be added by request.
Yes, we retain tooling and inspection fixtures for active programs. Inform us of your expected reorder schedule so we can plan storage and material readiness.
Inquiry Email
Include workpiece details, target holding force, quantity, and destination.